
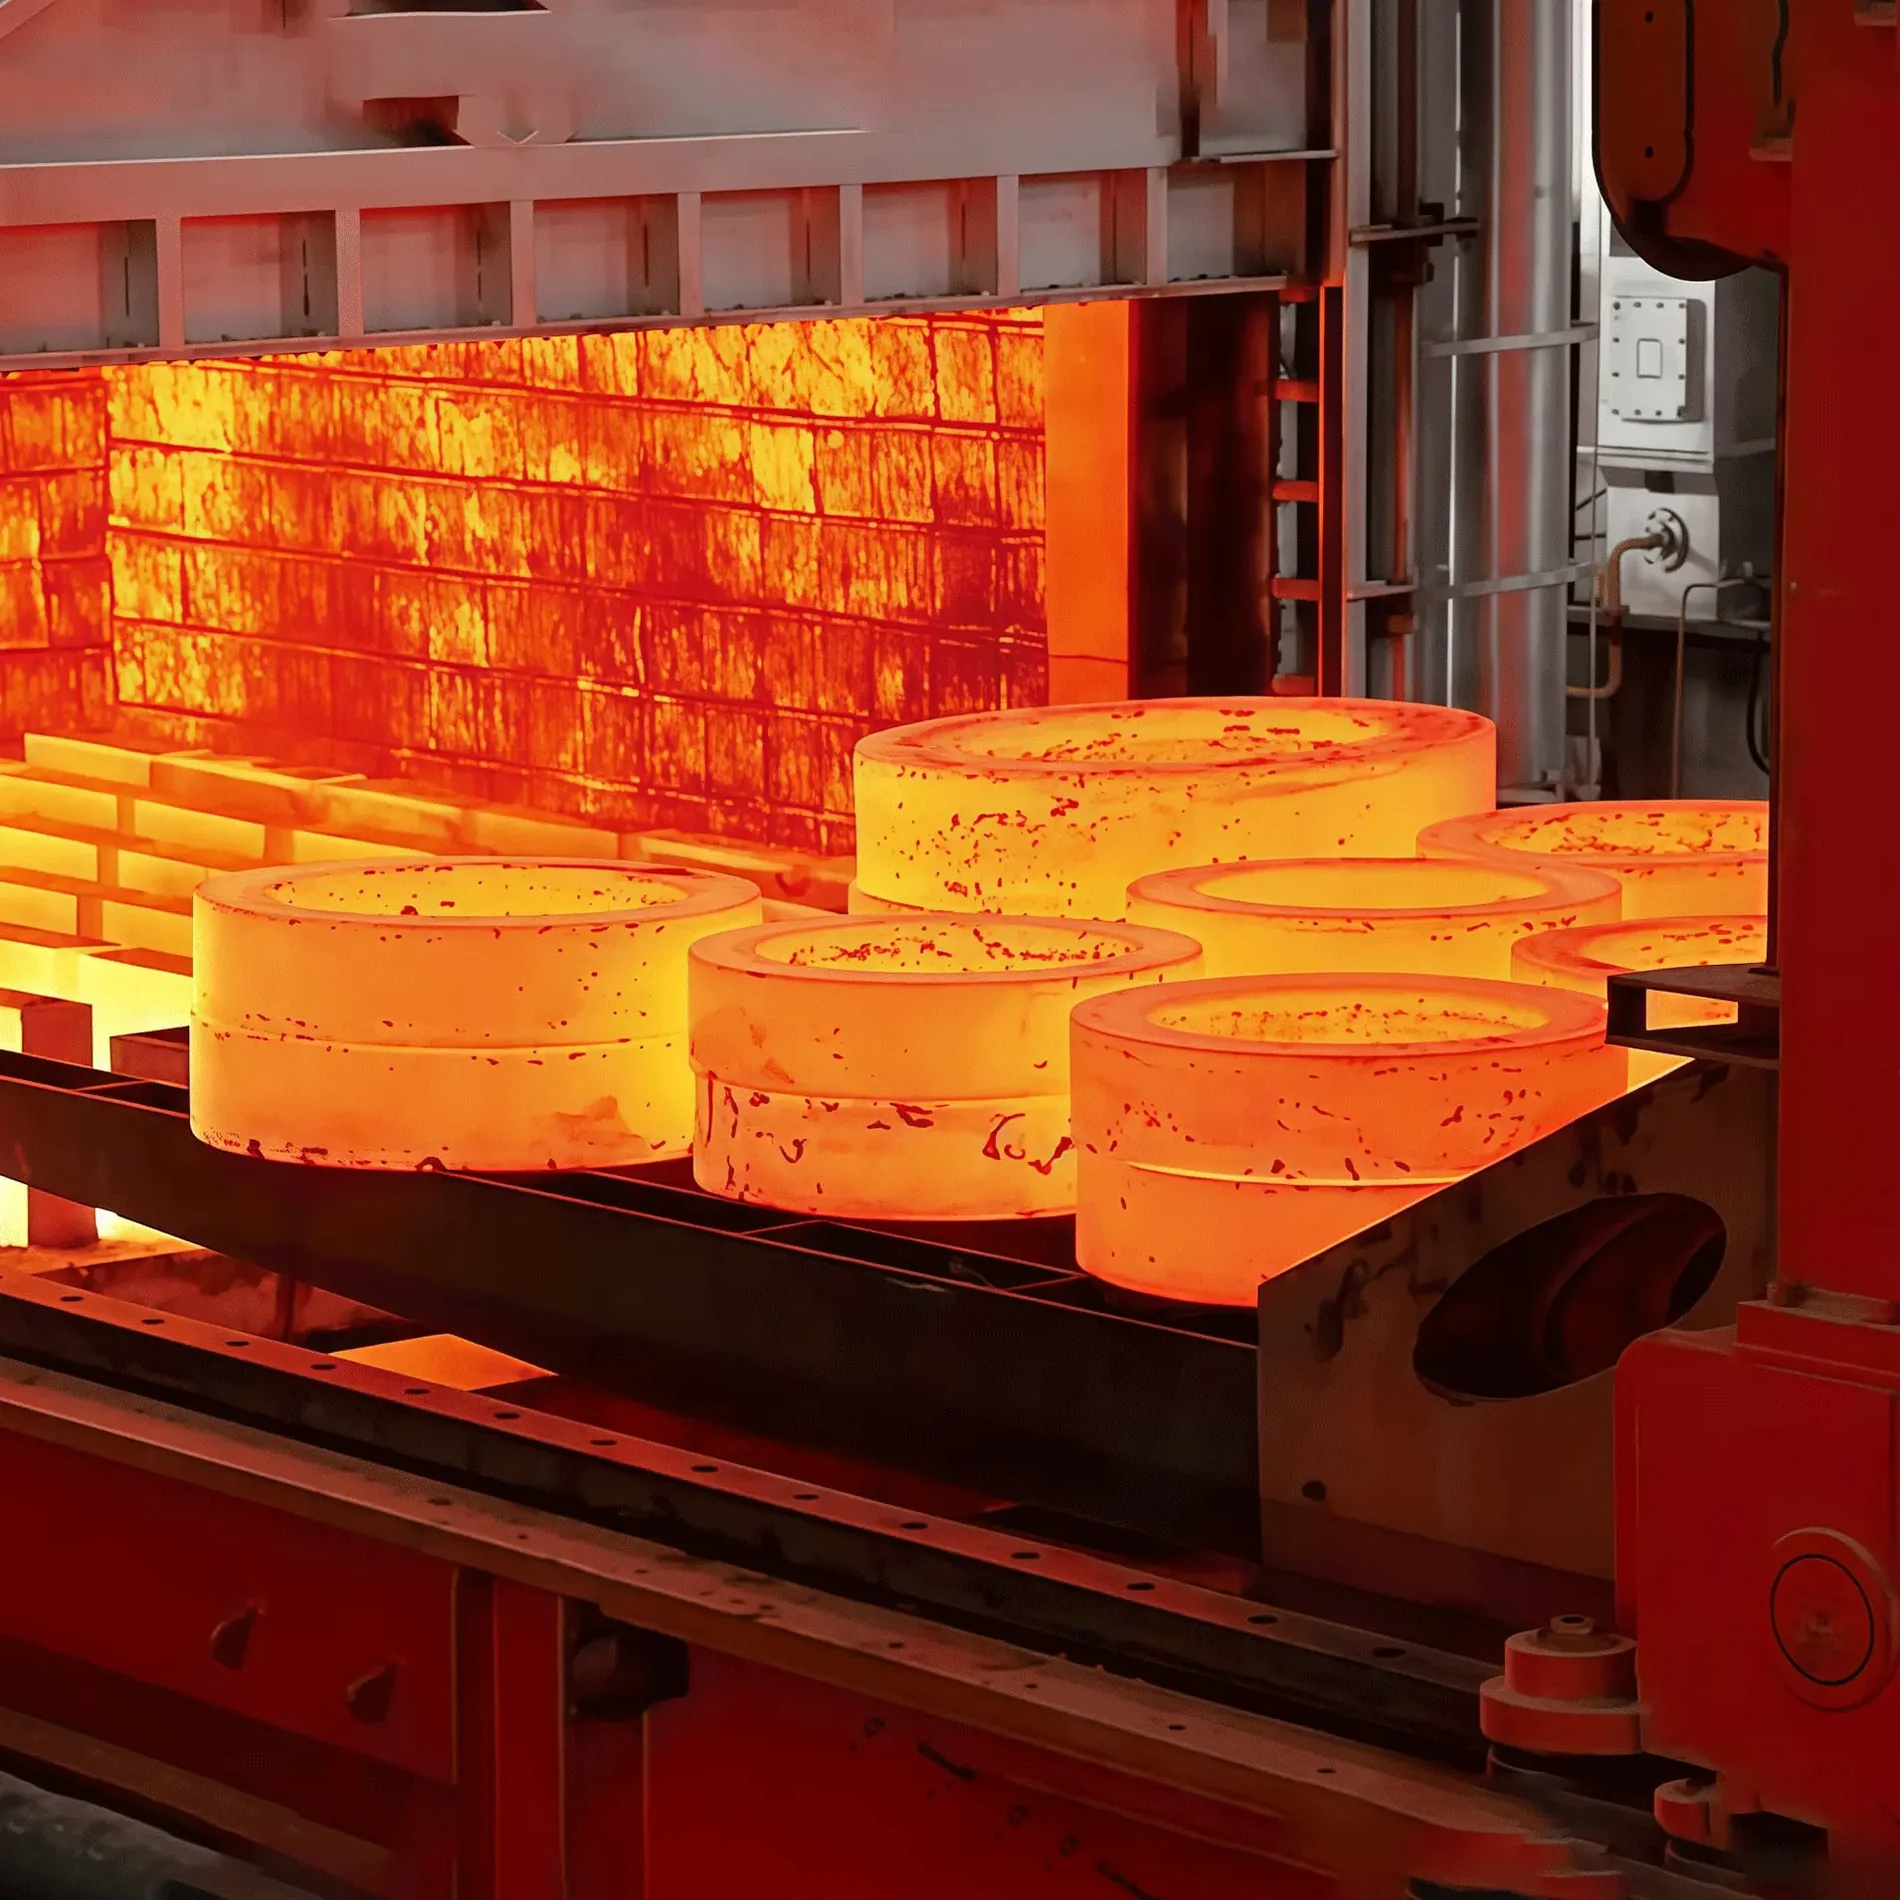
From Steelmaking to Very-Heavy Finished Forgings
A rare integrated manufacturing route combining steelmaking, secondary refining, very-heavy open-die forging, ring rolling, heat treatment, machining, inspection and project documentation for critical industrial components.
Heavy-Forgings.com is operated by REVROK for European and Middle East market development. Wuxi Hongda Heavy Industry is the current primary manufacturing partner.
Not just a large press — an integrated heavy-manufacturing route
Large forging capacity is only one part of the manufacturing problem. For critical pressure, energy, marine and mechanical components, the starting steel, ingot quality, forging ratio, heat treatment, machining envelope, NDT, inspection and final documentation all affect whether a component can be supplied successfully.
Hongda’s 2026 Changshu Hongteng facility adds steelmaking and a 160 MN open-die forging line to an established group already operating multiple forging presses, ring rollers, heat-treatment equipment, heavy machining, cladding, NDT and laboratory testing.
Steelmaking, secondary metallurgy and heavy forging
The new Changshu Hongteng plant has been in normal production since April 2026. Project-specific maximum dimensions and weights remain subject to material, geometry, forging route, heat treatment, machining and inspection requirements.
Primary melting route for special steels, integrated with secondary refining before ingot casting.
Ladle refining and vacuum degassing provide additional control over chemistry, gases and steel cleanliness.
Hongda’s current public plant information states stable casting of high-purity, high-density ingots up to 300 t single weight.
Electroslag equipment is listed within the current steelmaking section; use of a remelt route should be confirmed project by project.
160 MN / 16,000 t heavy forging line
| Capability | Technical detail | Commercial relevance |
|---|---|---|
| Press force | 160 MN / approximately 16,000 t | Very-heavy open-die forging and large-section deformation |
| Press clearance | Approx. 9.5 m | Accommodates very-large workpieces and tooling |
| Opening / column spacing | Approx. 9 m | Supports large-diameter and long heavy components |
| Manipulator | Imported German 600 T/M unit | Controlled handling and rotation during heavy forging sequences |
| Supporting facilities | Large heat-treatment furnaces and solution-treatment water pools | Supports integrated post-forging thermal processing |
| Project examples | Extra-large tube sheets, reactor shell rings, power rotors, marine crankshafts | Relevant to pressure, energy, marine and heavy-engineering sectors |
Note: final maximum forging weight and dimensions must be confirmed against the drawing and specification. Heavy-Forgings.com uses the 300 t class as a project-development capability, not as an unconditional limit for every geometry or material.
From ingot to inspected component
The buyer should evaluate the entire route rather than press size alone.

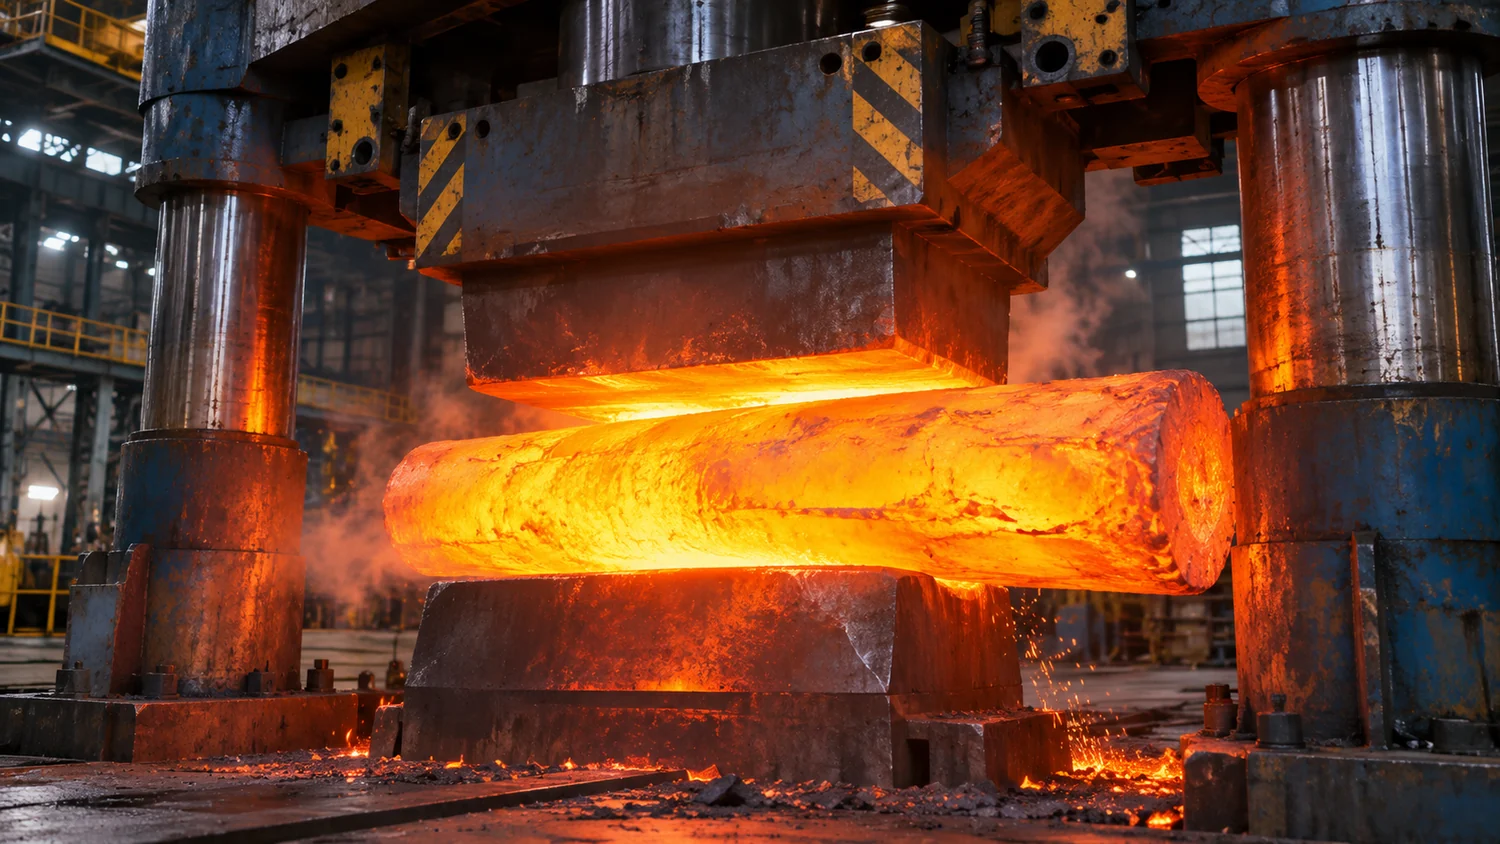
Open-Die Forging
Large engineered forgings to drawing, including critical pressure, shaft, rotor and machinery components.


Ring Rolling
Seamless ring production for pressure equipment, machinery, bearings, gear blanks and heavy circular components.

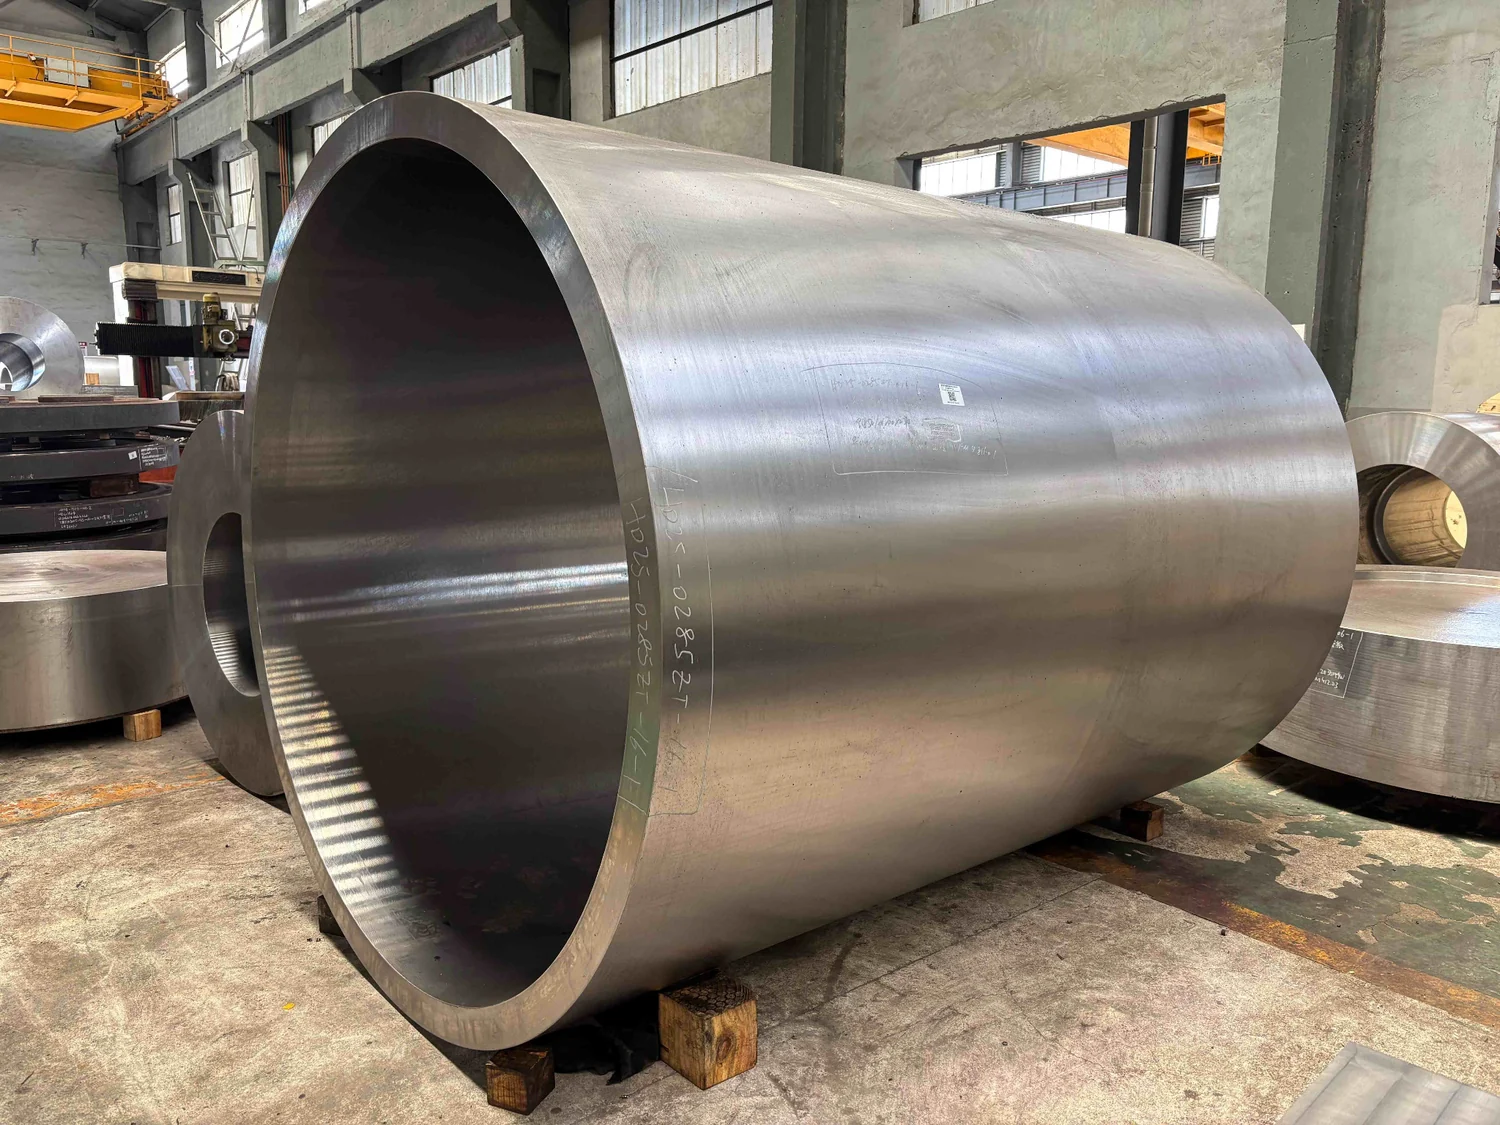
Heat Treatment & Machining
As-forged, rough-machined or finish-machined supply depending on drawing and project scope.
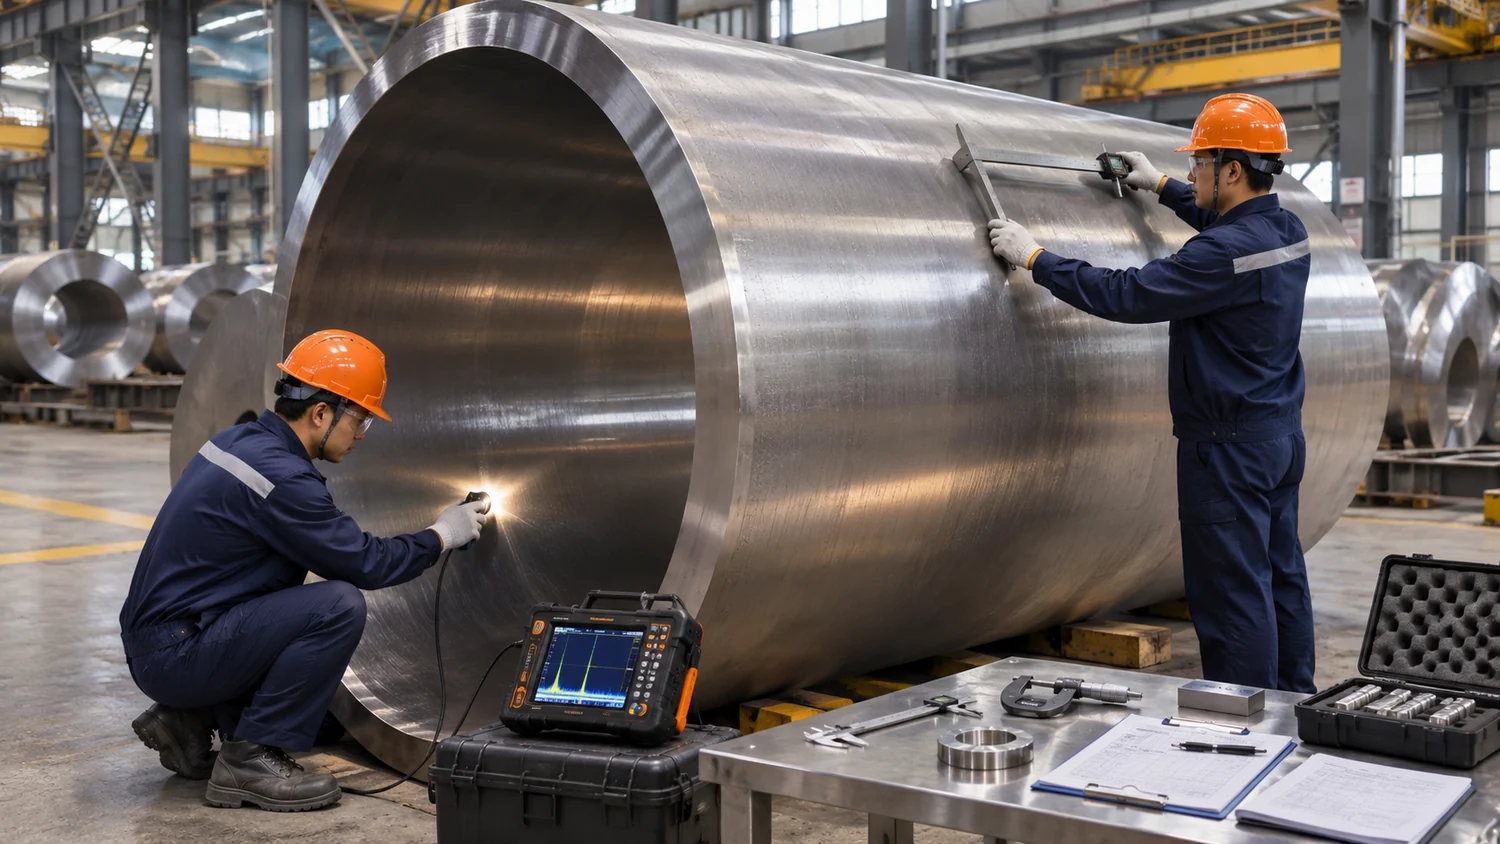
Inspection & Certification
Mechanical testing, metallography, UT, MT, dimensional inspection and project documentation.
Seamless rings, discs, shells and tube sheets
Rolled Rings
Established ring rolling includes 1.2 m, 3 m and 6 m equipment. Larger project dimensions should be reviewed against the new heavy-forging route and final geometry.
Tube Sheets
Large tube-sheet forging and drilling for heat exchangers, reactors, high-pressure heaters and process equipment. Current published drilling capability reaches approximately Ø7.5 m × 1 m thick.
Discs & Shells
Very-large discs, shell rings and cylindrical forgings can be evaluated for pressure, energy and heavy-equipment applications.
Machining capacity must match forging capacity
Hongda reports more than 100 sets of machining equipment.
| Operation | Published capability |
|---|---|
| Tube-sheet drilling | Up to approximately Ø7.5 m and 1 m thickness |
| Shaft deep-hole drilling | Approximately 10 m on the current public equipment page; other internal documentation references longer capability |
| Gantry machining | 9 m class gantry equipment; project envelope to be confirmed |
| General heavy machining | Sawing, turning, boring, milling, drilling, grinding |
| Cladding | CNC and manual cladding / weld-overlay capability for tube plates, cylinders and related components |
Large-component thermal processing
Large natural-gas furnace capacity for heating and heat-treatment cycles.
CNC-controlled electric furnaces for controlled thermal processing.
Vertical treatment route particularly relevant to long shafts and elongated forgings.
Water, oil and chemical quenching systems; project-specific cycle must match grade and required properties.
From pressure-vessel steels to nickel, titanium and high-temperature alloys
The material list is unusually broad for a group that also operates very-heavy open-die forging. Availability must always be confirmed against product form, size, melt route and certification scope.
| Material family | Representative grades / series |
|---|---|
| Carbon & structural steels | 10, 20, 35, 45, 55; Q355, Q390, Q420, Q460, Q690 |
| Pressure-vessel alloy steels | 16Mn(D), 20MnMo(D), 20MnMoNb, 20MnNiMo, 09MnNiD, SA105/SA266, SA350, SA508, SA765, F11, F22, F22V |
| Quenched & tempered alloy steels | 40Cr, 42CrMo, 34CrNiMo6, 30CrNiMo8, 36NiCrMo16 and related grades |
| Stainless steels | 304/304L, 316/316L, 317 and martensitic stainless families |
| Duplex & precipitation-hardening stainless | F51-type duplex families and PH stainless grades |
| Nickel alloys | Pure nickel, MONEL, INCONEL, INCOLOY, NIMONIC series |
| High-temperature alloys | Iron-, nickel- and cobalt-based high-temperature alloy families |
| Titanium & aluminium | TC/TA/TB titanium series and aluminium grades including 2214, 2A14, 5A06 |
Project-specific qualification rather than generic badges
Certification scope must be checked against the exact material, product form, size and project.
EU Pressure Equipment Directive capability for applicable pressure-equipment supply.
API certification listed by Hongda; project scope should be checked against the current certificate.
Multiple classification-society approvals including ABS, BV, DNV, NK, KR, LR, RINA and others.
Aerospace-related quality certification plus accredited laboratory / testing capability within the group.
Mechanical Testing
Room- and elevated-temperature tensile, hardness and other mechanical-property testing.
Metallurgical Testing
Metallography, drop-weight / drop-hammer related testing, endurance and end-quench capability.
NDT
Ultrasonic and magnetic-particle testing equipment plus project-specific inspection arrangements.
Technical entry points for buyers
Primary and authoritative reference links
Use these links to verify current equipment, materials, approvals and applicable European/API requirements.
Current public information on the 100 t EAF, LF + VD route, 160 MN press and 300 t ingot class.
Open-die presses, closed-die equipment, ring rollers, steelmaking, heat treatment, machining, cladding and testing.
Published carbon, pressure, alloy, stainless, duplex, nickel, high-temperature, titanium and aluminium grades.
Current public certificate portfolio including PED, API, marine, AS9100 and CNAS-related approvals.
Authoritative EU reference for PED 2014/68/EU.
Authoritative API standards resource; confirm the current applicable specification and certification scope.
Send the drawing, specification or initial requirement
REVROK will review the application, identify the relevant manufacturing route and coordinate technical clarification and quotation.
For very-large forgings, maximum dimensions and weights must be confirmed against material, geometry, heat treatment, machining and inspection requirements.